Food Manufacturing Yield: How Asian Producers Measure Raw-Material Efficiency and Process Loss
A food factory can produce every order on time and still use far more raw material than it should.
The problem is often hidden because the finished-product number receives most of the attention. If 10,000 packs leave the line, production appears successful. Yet that figure says very little about how much meat, fruit, flour, milk, sauce or other input was required to produce those packs, how much disappeared during processing, or whether the same quantity could have been produced with less material.
That is why food manufacturing yield deserves to be treated as an operating metric rather than an accounting calculation performed after the month has ended.
For Asian food manufacturers dealing with volatile ingredient prices, seasonal raw materials, labour constraints and increasingly complex product ranges, small changes in raw-material efficiency can affect both production cost and manufacturing capacity.
What Production Yield Actually Measures
At its simplest, production yield asks how much acceptable output a manufacturer obtains from a defined amount of input.
Basic production yield = acceptable finished output ÷ raw-material input × 100
If a plant receives 1,000 kg of raw material and produces 760 kg of acceptable finished product, the apparent yield is 76%.
But that number is only useful when the numerator and denominator have been defined consistently.
A food process changes material. Vegetables are peeled. Meat is trimmed. Water evaporates during heating. Ingredients may absorb water during cooking. Oil may be incorporated during frying. Bones, shells or seeds may legitimately leave the process. A product can also be rejected because it falls outside weight, appearance or quality specifications.
For that reason, an unusually high or low percentage does not by itself tell management whether a process is efficient.
The real question is:
How much output should this particular raw material, recipe and production process reasonably produce?
Not Every Lost Kilogram Is Waste
One of the most useful distinctions in food processing is between necessary transformation and unwanted process loss.
Consider a manufacturer producing peeled fruit pieces. Skin and seeds may be expected to leave the saleable product. A sauce manufacturer may deliberately evaporate water until a target concentration is reached. A meat processor may remove bone, fat or damaged tissue according to specification.
Those losses are fundamentally different from:
- excessive trimming;
- product left inside transfer pipes;
- overfilling packs;
- incorrect equipment settings;
- damaged product during handling;
- rejects caused by inconsistent processing;
- spillage;
- incorrect cooking time;
- unrecorded rework;
- material written off because stock records do not match physical usage.
Production-yield research has long distinguished between losses required to transform raw material into the intended product and avoidable losses that unnecessarily consume material.
That distinction should also shape factory reporting.
The Five-Bucket Yield Model
Instead of recording only input and final output, divide the material flowing through a production run into five buckets.
| Bucket | What It Includes | Management Question |
|---|---|---|
| Saleable output | Finished product meeting specification | How much material became something we can sell? |
| Necessary transformation | Peels, bones, evaporation or other expected process change | Is this loss inherent to the specification? |
| Recoverable material | Trim, offcuts or by-products that can legitimately enter another approved process | Are we recovering value safely and consistently? |
| Quality loss | Rejects, damaged packs, out-of-specification product | Which process condition created the failure? |
| Unexplained variance | Material that cannot be reconciled through production records | Where did it go? |
The last category is particularly important.
A plant can debate acceptable trimming standards. It cannot manage an unexplained difference between what entered the process and what its records say left it.
A good mass-balance exercise therefore attempts to account for the whole batch, not merely the finished cartons.
Measure Yield at More Than One Point
A single factory-level yield percentage can hide where the problem occurs.
Imagine a frozen snack line with six stages:
- raw-material receiving;
- preparation and trimming;
- mixing or forming;
- cooking;
- freezing;
- packing.
If the final yield declines, management needs to know whether more material was lost during trimming, cooking, freezing or packing.
This is why useful yield analysis follows the material through critical process stages.
Record the weight entering a stage, the acceptable output leaving it, known by-products, rejects and any additions such as water, oil, coating or other ingredients.
The objective is not to create paperwork around every movement. It is to identify the points where relatively small measurement differences can expose relatively large financial losses.
Build a Standard Yield Before Chasing Variance
Managers sometimes set a yield target by taking last month’s result and asking for one percentage point more.
That is not a standard. It is an aspiration.
A defensible standard yield should reflect the actual process and product specification. Useful inputs include:
- raw-material grade and condition;
- ingredient specification;
- recipe formulation;
- normal trim requirements;
- cooking or drying conditions;
- finished moisture or solids specification;
- portion and pack-weight limits;
- equipment capability;
- acceptable rework rules;
- historical performance from stable production runs.
Seasonal ingredients may need more than one baseline.
A fruit processor, for example, should not automatically expect identical usable yield from raw material arriving at different maturity levels, sizes or moisture conditions. If purchasing quality changes, operations should know whether the yield movement reflects factory execution or a different input.
Watch Giveaway as Closely as Scrap
One of the least dramatic forms of manufacturing loss is also one of the easiest to miss: giving customers more product than the specification requires.
A pack labelled at a defined net quantity needs sufficient process control to meet applicable requirements. But consistently operating far above the required fill level consumes material without creating additional saleable units.
Suppose one line routinely fills slightly heavier than another. Both may produce compliant packs. The heavier line nevertheless converts the same quantity of raw material into fewer units.
The problem is not solved by simply lowering fill weights. Food businesses must continue to satisfy legal and quality requirements. The operating objective is tighter variation around an appropriate target.
That usually makes process consistency more valuable than simply instructing operators to “use less”.
Separate Yield From Throughput
Fast production is not necessarily efficient production.
A line can increase output per hour while reducing raw-material yield if faster operation causes more breakage, inaccurate cutting, poor filling or quality rejects.
Management should therefore view at least three dimensions together:
- Throughput: how much product is produced over time;
- Yield: how effectively input becomes acceptable output;
- Quality: whether that output actually meets specification.
Optimising one while ignoring the other two can create misleading improvements.
The same principle applies when evaluating new machinery. A faster filler, cutter or forming line should not be justified only by theoretical capacity. The business should also understand material loss, giveaway, rejects, cleaning loss, changeover loss and consistency under normal production conditions.
The Yield Variance Investigation
When actual yield falls below standard, avoid starting with a vague instruction to reduce waste.
Use a structured investigation.
1. Confirm the Measurement
Check whether the batch boundaries, scales, production records and units are correct. An apparent production problem may be a recording problem.
2. Check Raw-Material Variation
Compare supplier, grade, moisture, size, maturity, temperature and other relevant input characteristics with normal batches.
3. Locate the Stage
Identify where the variance first appears rather than treating the entire line as one process.
4. Separate Planned From Unplanned Loss
Determine whether the difference is explained by legitimate transformation or represents avoidable loss.
5. Check Process Conditions
Review settings, temperatures, time, speed, blade condition, calibration, pressure, operator method and other variables relevant to the process.
6. Examine Rejects and Rework
A process can appear to have acceptable output when large quantities are repeatedly being reworked. Track rework separately so it does not hide first-pass performance.
7. Verify Finished Specification
A higher yield is not an improvement if it was achieved by changing moisture, portion size, concentration or another product characteristic outside the approved specification.
A Practical Yield Dashboard
Food manufacturers do not need dozens of production indicators to begin.
| Measure | Why It Matters |
|---|---|
| Raw-material input | Establishes the denominator for the batch |
| Saleable output | Shows how much acceptable product was created |
| Actual yield | Measures conversion efficiency |
| Standard yield | Provides a meaningful comparison |
| Yield variance | Shows the gap requiring investigation |
| Reject quantity | Separates quality failure from normal transformation |
| Giveaway | Identifies excess material delivered without additional revenue |
| Rework quantity | Shows how much production required a second processing cycle |
| Unexplained material variance | Highlights gaps in physical or record control |
Reviewing these measures by product, line, shift, raw-material lot or supplier can reveal patterns that a monthly factory average will conceal.
Do Not Confuse Yield Improvement With Food-Safety Shortcuts
Production efficiency does not override food safety, product quality, regulatory requirements or required processing conditions.
A factory should never improve apparent yield by retaining material that should be rejected, reducing required processing, using prohibited rework, changing ingredient specifications without approval or bypassing controls.
Documentation remains particularly important in food production. FAO guidance on HACCP record keeping emphasises maintaining records sufficient to demonstrate that relevant controls are operating and being maintained.
Yield optimisation therefore needs to sit inside the established food-safety and quality system rather than operate around it.
When Production Data Becomes Evidence of a Larger Achievement
For most manufacturers, yield is simply a management tool. Improving raw-material efficiency is valuable because it improves the operation, not because every improvement deserves outside recognition.
Over time, however, a food business may accumulate evidence of an objectively unusual achievement: a defined production volume, an exceptional number of qualifying products, a measurable output milestone or another clearly bounded F&B result.
That is a different question from normal factory performance.
Businesses investigating record recognition in Asia should begin with the same discipline used in production control: define exactly what happened, identify the unit of measurement and preserve the underlying evidence.
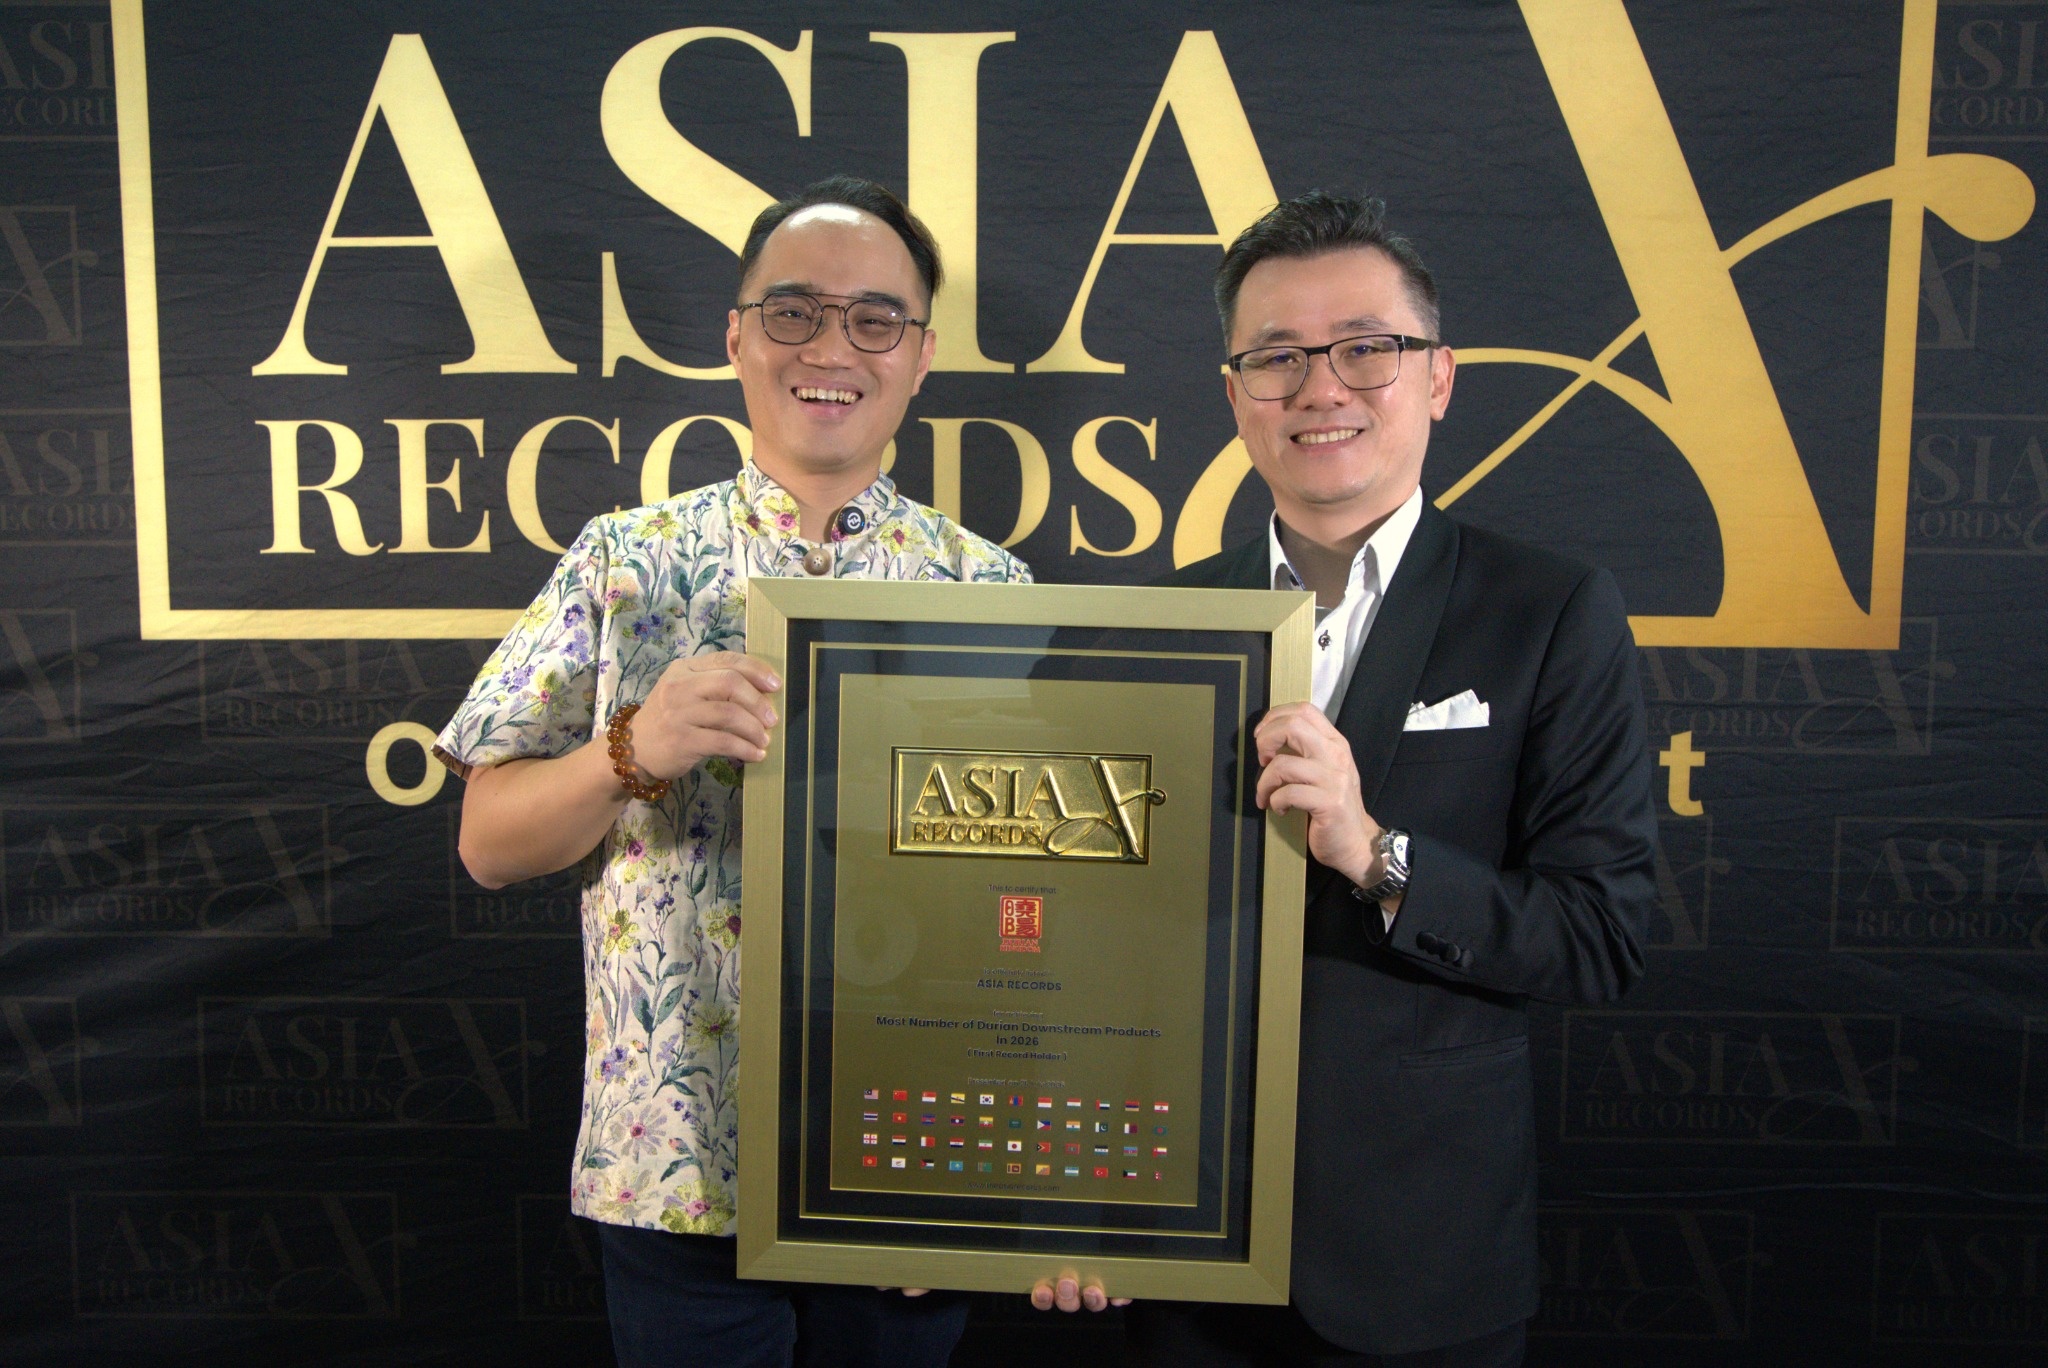
The Asia Record official application process states that individuals, businesses, organisations and institutions may propose a measurable achievement and provide supporting evidence for assessment and verification.
For a manufacturer researching an Asia record application, how to get an Asia Record or whether it could apply for Asia Record, reliable production documents can therefore be more important than promotional material. If an achievement is approved, the business may become an Asia Record holder, but record recognition remains separate from food-safety certification, regulatory approval, halal certification or other compliance requirements.
Asia record certification should document an eligible measurable achievement; it should never be presented as proof that a food product satisfies regulatory or technical standards it was not designed to assess.
The Factory Question Worth Asking Every Week
Food manufacturing efficiency is not simply about producing more.
It is about understanding what happened to the material already purchased.
How much became saleable food? How much changed because the process required it? How much became a legitimate by-product? How much was rejected? How much was given away through excessive variation? And how much cannot be explained at all?
Once those questions can be answered consistently, production yield stops being a percentage at the bottom of a spreadsheet.
It becomes a map of where the factory is creating value — and where that value is disappearing.